
10 Leading 16% aluminum sulphate Manufacturers in the world 2025
Sep 23, 2025
Leave a message
Introduction to 16% Aluminum Sulphate
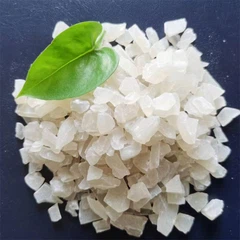
Aluminum sulphate with a 16% concentration is a widely used chemical compound. It is commonly employed in water treatment processes to clarify water by removing suspended particles and impurities. In the paper industry, it acts as a sizing agent to improve the paper's strength and printability. Additionally, it finds applications in the textile industry for dyeing and printing, as well as in the production of various other chemicals. The 16% concentration is a standard specification that meets the requirements of many industrial applications due to its balanced chemical properties and effectiveness.
10 Leading Manufacturers
1. Zibo Guangzheng Aluminum Sulphate Salts Co., Ltd
Zibo Guangzheng Aluminum Sulphate Salts Co., Ltd is a prominent player in the global aluminum sulphate market. Located in Zibo, a region known for its rich chemical industry resources in China, the company has been dedicated to the production and research of aluminum sulphate for many years.
The company has a state - of - the - art production facility that adheres to strict quality control standards. Their production process is highly efficient, making use of advanced technology to ensure the consistency and purity of their 16% aluminum sulphate products. They source high - quality raw materials and have a well - trained team of technicians and chemists who monitor every step of the production process.
In terms of the 16% aluminum sulphate they produce, it has excellent flocculation properties, which makes it highly effective in water treatment. The product can quickly and efficiently remove suspended solids, colloids, and some heavy metals from water, improving water quality. The company also offers customized packaging options to meet the different needs of customers, whether it is for small - scale local water treatment plants or large - scale industrial users.
One of the key advantages of Zibo Guangzheng Aluminum Sulphate Salts Co., Ltd is its strong R & D capabilities. They continuously invest in research to improve the performance of their products and develop new applications for 16% aluminum sulphate. Moreover, the company has a wide distribution network that allows them to supply their products to customers all over the world in a timely manner. Their customer service is also highly praised, with a professional team ready to provide technical support and after - sales service.Website: https://www.alumsulphate.com/
2. Kemira Oyj
Kemira Oyj is a Finnish chemical company with a long - standing reputation in the global market. Established in 1920, it has grown into a major player in the specialty chemicals industry. The company operates in more than 40 countries and has a diverse product portfolio that includes water treatment chemicals, pulp and paper chemicals, and oil and gas chemicals.
For their 16% aluminum sulphate production, Kemira uses advanced manufacturing processes that ensure high - quality and consistent products. Their focus on sustainable development is evident in their production methods, which aim to minimize environmental impact. In the water treatment sector, their 16% aluminum sulphate is known for its ability to work effectively in a wide range of water conditions, including different pH levels and water temperatures.
Kemira's 16% aluminum sulphate is also highly valued in the pulp and paper industry. It helps in improving the retention of fillers and fines, which in turn enhances the quality of the paper. The company has a large - scale production capacity, which allows them to meet the high - volume demands of industrial customers. Their strong technical support team provides on - site assistance to customers, helping them optimize the use of their products and solve any technical problems.One of the main advantages of Kemira is its global presence. This enables them to quickly respond to the needs of customers around the world. They also have a deep understanding of local markets, which allows them to tailor their products and services according to regional requirements.
3. Occidental Chemical Corporation (OxyChem)
Occidental Chemical Corporation, or OxyChem, is a leading North American manufacturer and marketer of basic chemicals, vinyls, and performance chemicals. Headquartered in Dallas, Texas, the company has a long history of innovation and excellence in the chemical industry.
OxyChem's 16% aluminum sulphate production is characterized by its strict quality control. They have a comprehensive quality management system in place that ensures every batch of products meets the highest standards. Their product is widely used in water treatment, where it is recognized for its high - speed flocculation and excellent sedimentation properties.In addition to water treatment, OxyChem's 16% aluminum sulphate is used in the production of various consumer products. The company has a large research and development center where scientists are constantly working on improving the product's performance and exploring new applications.One of the key advantages of OxyChem is its integration of the supply chain. They have access to reliable sources of raw materials, which helps in maintaining stable production and competitive pricing. Their strong brand reputation also gives them an edge in the market, as customers trust the quality and reliability of their products.
4. GEO Specialty Chemicals
GEO Specialty Chemicals is a global specialty chemicals company that focuses on serving various industries, including water treatment, pulp and paper, and agriculture. The company has a wide range of manufacturing facilities located around the world, which allows it to efficiently produce and distribute its products.For their 16% aluminum sulphate, GEO Specialty Chemicals emphasizes product customization. They understand that different customers have different requirements, so they can adjust the product's properties according to specific needs. In water treatment, their product can be formulated to be more effective in treating water with high levels of organic matter or certain contaminants.The company also has a strong commitment to environmental protection. Their production processes are designed to minimize waste and energy consumption. GEO Specialty Chemicals' 16% aluminum sulphate is also known for its long - term stability, which means it can be stored for a longer time without significant degradation of its properties.One of the advantages of GEO Specialty Chemicals is its close relationship with customers. They work closely with clients to understand their problems and develop solutions. Their technical experts are always available to provide advice and support, which helps customers optimize the use of their 16% aluminum sulphate.
5. Aditya Birla Chemicals
Aditya Birla Chemicals is part of the Aditya Birla Group, one of the largest conglomerates in India. The company has a significant presence in the global chemical market, with manufacturing facilities in multiple countries.In the production of 16% aluminum sulphate, Aditya Birla Chemicals leverages its large - scale production capabilities. They can produce high - volume products at a relatively low cost, which gives them a competitive advantage in the market. Their product is widely used in the water treatment industry in Asia, where it has been proven to be effective in treating different types of water sources.The company also invests in research and development to improve the quality of its 16% aluminum sulphate. They are constantly exploring new ways to enhance the product's performance, such as increasing its flocculation efficiency and reducing its environmental impact.Aditya Birla Chemicals' advantage lies in its strong brand image in the Asian market. They have a well - established distribution network in the region, which allows them to quickly deliver products to customers. Their local knowledge and understanding of the Asian market also enable them to better meet the specific needs of customers in this area.
6. Nouryon
Nouryon, formerly AkzoNobel Specialty Chemicals, is a global specialty chemicals company with a focus on sustainable solutions. The company has a long history of innovation and is committed to developing products that are environmentally friendly and socially responsible.For their 16% aluminum sulphate, Nouryon uses advanced production technologies that ensure high - purity products. Their product is widely used in the water treatment industry, where it is known for its ability to remove phosphorus from water, which is crucial for preventing eutrophication in water bodies.Nouryon also has a strong R & D team that is working on developing new applications for 16% aluminum sulphate. They are exploring its use in emerging industries, such as the bio - energy sector. The company's commitment to sustainability is reflected in its production processes, which aim to reduce carbon emissions and waste generation.One of the advantages of Nouryon is its global reach and strong customer relationships. They have a presence in many countries and work closely with customers to understand their needs and provide customized solutions. Their technical support and after - sales service are also highly regarded in the market.
7. Solvay
Solvay is a Belgian chemical company that has been operating for over 150 years. It is a global leader in advanced materials and specialty chemicals, with a diverse product portfolio that serves various industries, including automotive, aerospace, and water treatment.Solvay's 16% aluminum sulphate production is characterized by its high - quality standards. They use state - of - the - art manufacturing facilities and strict quality control measures to ensure the consistency and purity of their products. In the water treatment industry, their product is known for its excellent performance in removing turbidity and color from water.The company also has a strong R & D focus, with a team of scientists working on improving the properties of 16% aluminum sulphate. They are exploring new ways to make the product more effective in treating complex water systems, such as those with high levels of heavy metals or organic pollutants.Solvay's advantage lies in its global brand recognition and technical expertise. Their long - standing reputation in the chemical industry gives customers confidence in their products. They also have a wide range of technical services available, including water analysis and process optimization, which helps customers get the most out of their 16% aluminum sulphate.
8. Tata Chemicals
Tata Chemicals is an Indian company that is part of the Tata Group, one of India's most respected business conglomerates. The company has a significant presence in the global chemical market, with operations in multiple countries.For their 16% aluminum sulphate, Tata Chemicals has a well - established production process. They source high - quality raw materials and use advanced manufacturing techniques to produce a product that meets international standards. Their product is widely used in the water treatment industry in India and other Asian countries, where it has been proven to be effective in treating different types of water sources.The company also invests in research and development to improve the performance of its 16% aluminum sulphate. They are working on developing new formulations that can be more effective in treating water with specific contaminants. Tata Chemicals' advantage lies in its strong local presence in India and other Asian markets. They have a deep understanding of the local needs and can provide customized solutions to customers. Their large - scale production capacity also allows them to meet the high - volume demands of the market.
9. BASF SE
BASF SE is the world's largest chemical company, based in Germany. It has a diverse product portfolio that covers a wide range of industries, including agriculture, automotive, and water treatment.In the production of 16% aluminum sulphate, BASF uses its advanced chemical engineering expertise. They have a large - scale production facility that can produce high - quality products in large quantities. Their product is known for its excellent stability and performance in water treatment applications.BASF also has a strong R & D department that is constantly working on improving the product's properties. They are exploring new applications for 16% aluminum sulphate, such as in the field of environmental remediation. The company's advantage lies in its global reach and comprehensive technical support. They have a network of experts around the world who can provide on - site assistance to customers and help them optimize the use of their products.
10. FMC Corporation
FMC Corporation is an American chemical company that specializes in agricultural sciences, health and nutrition, and industrial chemicals. The company has a long history of innovation and is committed to providing sustainable solutions to its customers.For their 16% aluminum sulphate, FMC Corporation has a unique production process that ensures high - purity products. Their product is widely used in the water treatment industry, where it is known for its ability to remove a wide range of contaminants, including bacteria and viruses.The company also invests in research to develop new applications for 16% aluminum sulphate. They are exploring its use in the food and beverage industry for water treatment purposes. FMC Corporation's advantage lies in its strong R & D capabilities and its focus on sustainable development. Their products are designed to have a minimal environmental impact while still providing high - performance solutions.
Summary
The 10 leading 16% aluminum sulphate manufacturers in the world in 2025 represent a diverse group of companies from different regions. Each company has its own unique strengths and characteristics. Some, like Zibo Guangzheng Aluminum Sulphate Salts Co., Ltd, offer customized products and strong R & D capabilities. Others, such as Kemira Oyj and BASF SE, have a global presence and comprehensive technical support. These manufacturers play a crucial role in meeting the global demand for 16% aluminum sulphate, which is widely used in various industries, especially water treatment. As the demand for high - quality water and sustainable chemical products continues to grow, these companies are likely to further invest in research and development to improve their products and expand their market share. Their combined efforts will contribute to the continuous development and innovation in the 16% aluminum sulphate industry.
Send Inquiry